Recurring job list
List sheet sizes, fold drawings, paper stocks and typical batch quantities.
Selection decision: Choose the platform and plate arrangement around the jobs you regularly quote.
Solution · Commercial print
Choose a folding configuration for the production mix: brochures, mailers and inserts, with changeover and delivery planned alongside speed.
Production brief
A commercial print finisher is judged on the number of different jobs that can leave the floor in a day. That makes changeover time, fold-pattern range and the ability to switch paper stock between jobs more important than a headline speed figure nobody runs all week.
The SPEED commercial configuration is a buckle folder with enough plates to reach every standard pattern from one setup. A 10+4 or 12+6 machine covers parallel, letter, gate, accordion and cross folds; when a job needs a knife fold, a combination (buckle + knife) model runs it in a single pass — ask us for the current combination range.
Published configuration references · Ratings depend on the model and configuration; they are not an accepted-output guarantee for a complete line.
01 / Define the job
Start with the printed piece and the production requirement. These details help our team compare equipment and propose the process.
List sheet sizes, fold drawings, paper stocks and typical batch quantities.
Selection decision: Choose the platform and plate arrangement around the jobs you regularly quote.
Show whether pieces go to packing, gathering, stitching or another operation.
Selection decision: Specify delivery and any additional finishing interfaces for the workflow.
Provide two or three common consecutive jobs and their required turnaround.
Selection decision: Assess setup, first accepted output and operator tasks across the actual job mix.
State campaign volumes, shift time and constraints on loading or collection.
Selection decision: Review feed continuity and accepted output during the busiest production periods.
Production requirements and the specification decisions to review for this folding job.
Buckle plates are adjustable stops, so a change between a tri-fold leaflet and a gate-fold brochure is a plate reposition, not a tooling change. The plate count you specify decides how many patterns you can reach without re-threading the machine.
A commercial floor runs 80 gsm offset in the morning and 250 gsm cover board in the afternoon. Suction-wheel separation, double-sheet detection and adjustable creasing pressure let the feeder and rollers be set to the job rather than to an average.
Some patterns — a right-angle fold on heavy cover stock, for example — are cleaner on a knife than on a buckle. A combination machine carries both principles so the job does not have to move to a second machine.
Direct-mail campaigns arrive in bursts. A 750 mm pile, a round-pile feeder and 180 m/min sustained running absorb the spike without a second shift on the folder.
02 / Plan the process
A process reference for the project discussion. The final layout and optional stages are agreed from the job drawing and sample run.
Review the printed sheet and set the feeding and folding arrangement.
Run the selected brochure, mailer or insert pattern using the agreed stock.
Match stack presentation to packing or the next print-finishing operation.
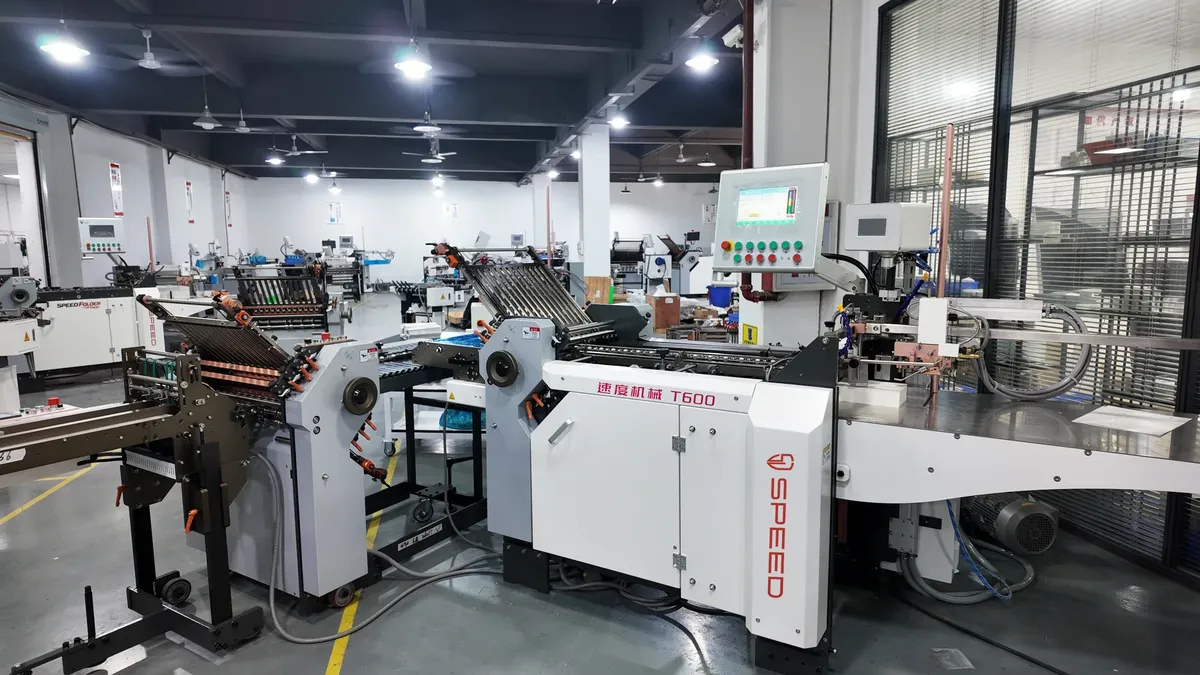
T600 (600 × 1000 mm, 750 mm pile, 180 m/min) as the volume platform; a combination buckle-and-knife model where those folds are needed in one pass.
10+4, 12+6 or 14+6 plate sets. Choose on the pattern list you actually quote, not on the maximum available.
Servo automatic feeder as standard; round-pile feeder on the T600 platform for direct-mail volumes.
Vertical stacker for small folded panels and mailers; standard belt delivery for brochure and catalogue formats.
03 / Select the equipment
Compare the linked equipment by its role. Folders and finishing modules are selected for their own operating envelope; every unit is not required for every job.
Commercial production folding
Compare sheet format, fold arrangement and delivery requirements across the regular job mix.
View specifications →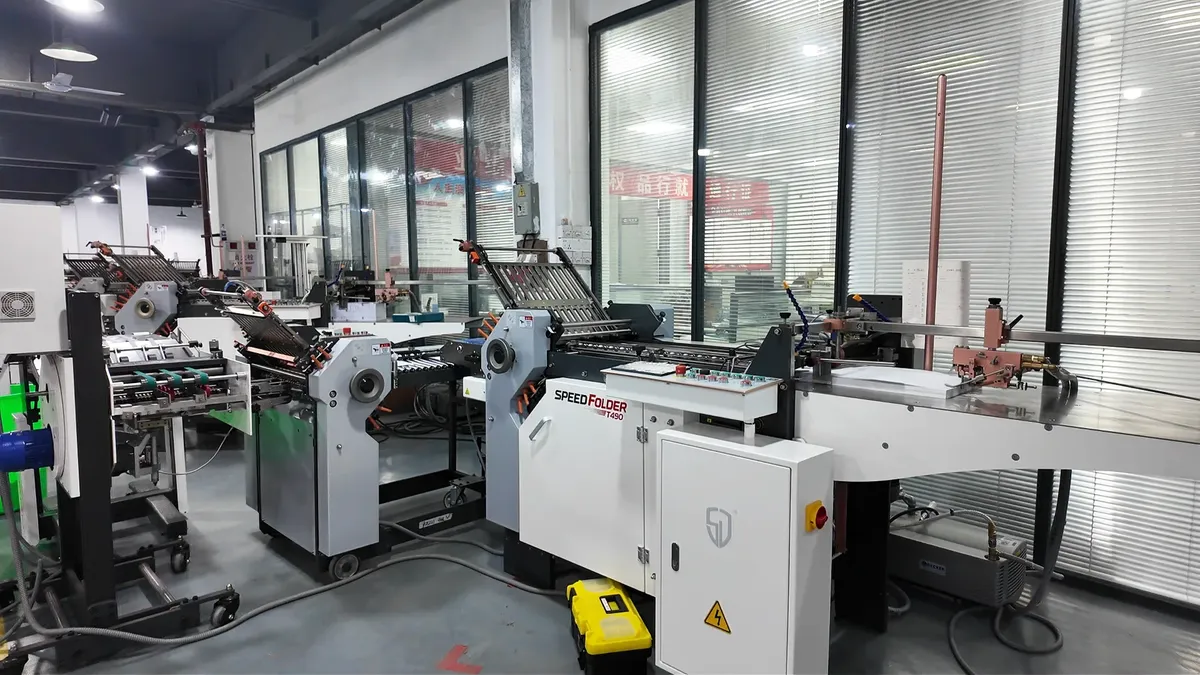
Miniature buckle folding
Review the minimum sheet and finished panel size for small leaflets and inserts.
View specifications →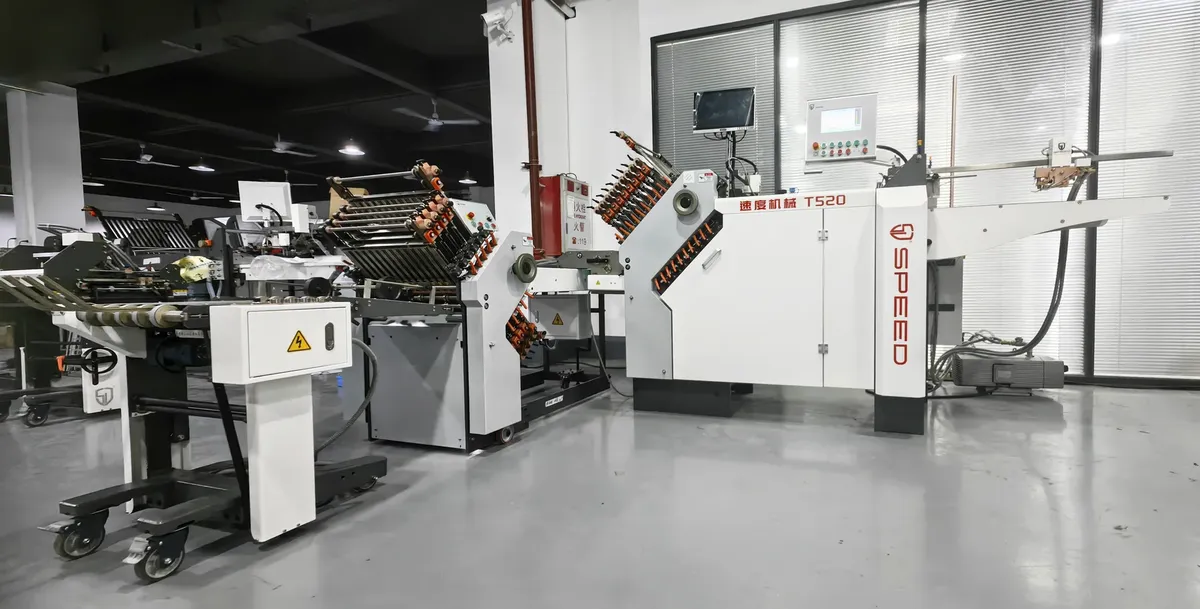
Leaflet folding and line integration
Review the leaflet format and the interfaces to trimming, pressing and delivery equipment.
View specifications →| Equipment | Sheet / feed / working width | Paper weight / finished thickness | Published speed |
|---|---|---|---|
| T600 | 600 × 1000 mm | 28–200 gsm | 180 m/min |
| T490 | 490 × 1000 mm | 28–200 gsm | 180 m/min |
| T520 | 520 × 1000 mm | 28–200 gsm | 180 m/min |
Values refer to individual products. Actual line output depends on the stock, fold sequence, optional equipment and delivery arrangement.
Use the diagrams to describe the finished piece. The model references below come from the reviewed product overviews; the ordered plate arrangement and your stock determine the final fold capability.
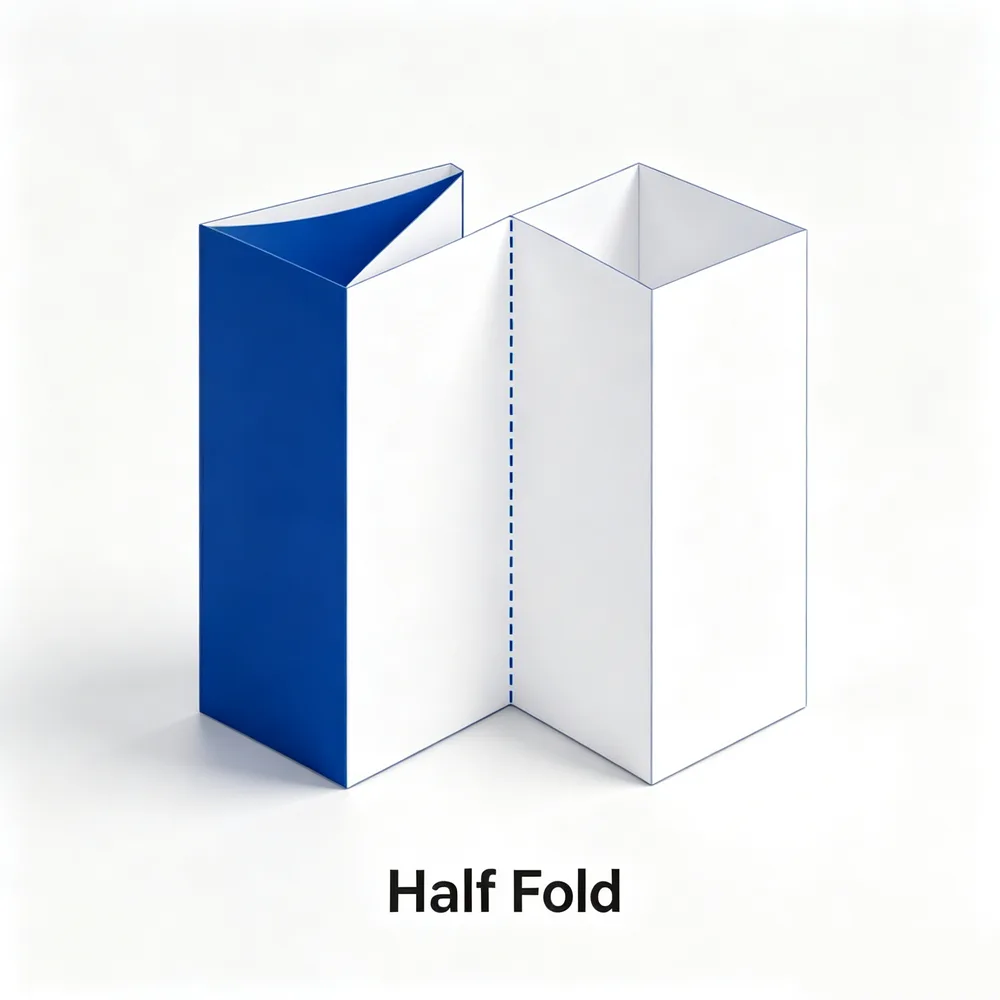
One fold, two panels — leaflets, mailers, greeting cards.
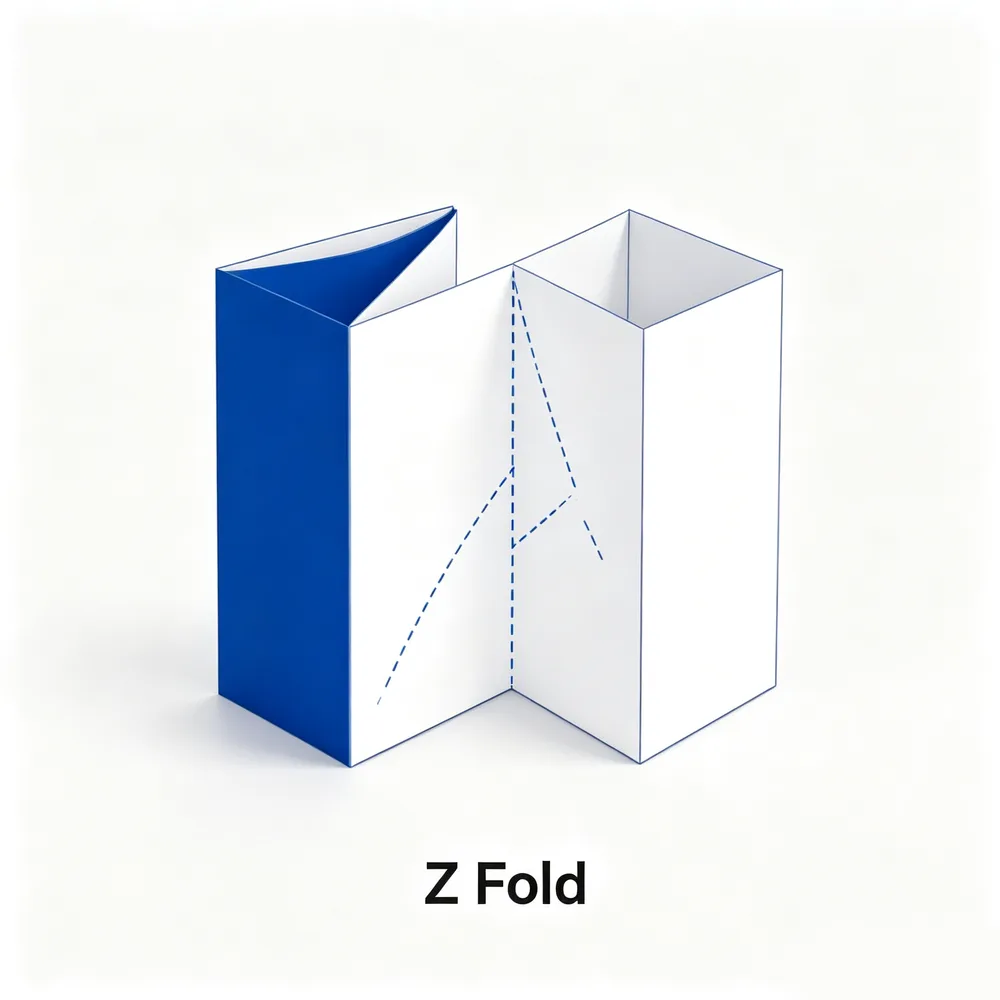
Parallel fold lines alternate so the sheet opens in a zig-zag.
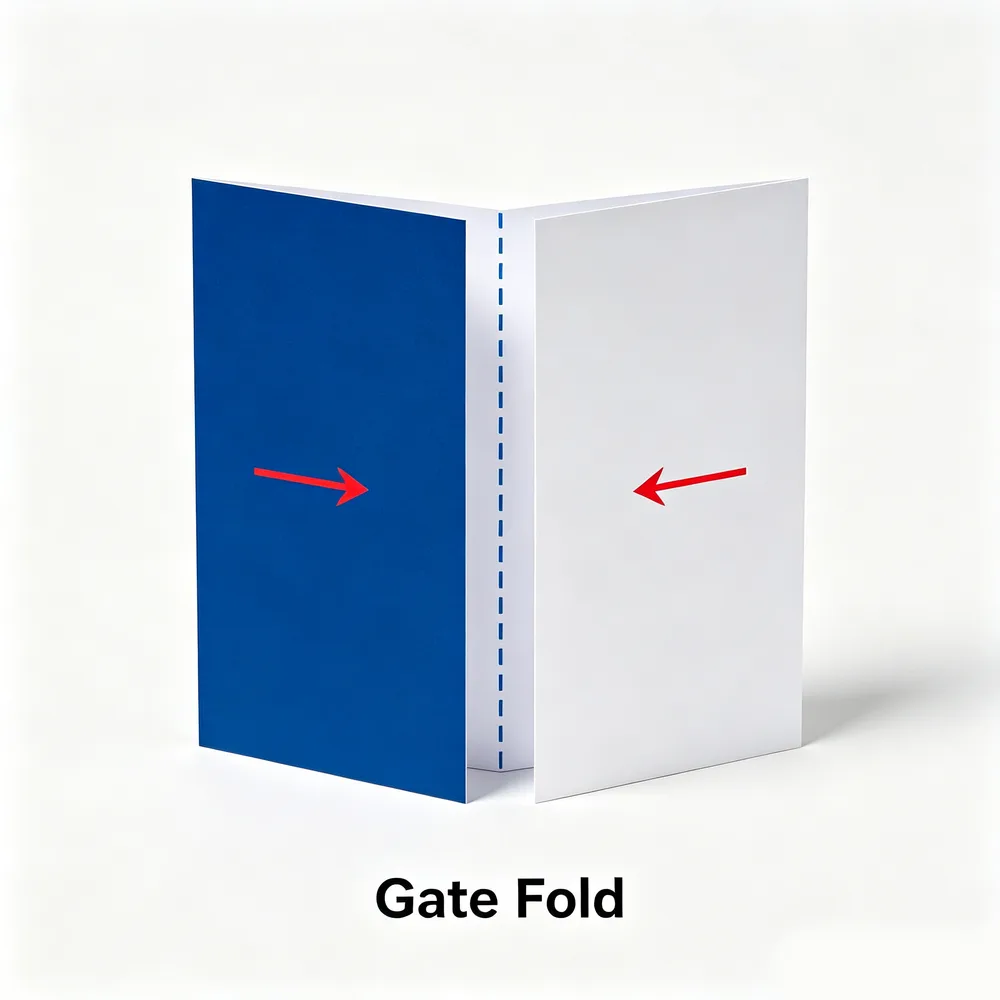
Two panels fold inward and meet in the centre — the classic programme insert.
View the related feeding, folding or finishing operation in the existing SPEED video library. Confirm the proposed configuration against your own job brief.
Booklet & brochure buckle folder in production
A T600-class buckle folder running multi-panel booklet and brochure folds — plate changeover, roller grip and stacker delivery shown end to end.
Watch on YouTube →Automatic industrial booklet folding at speed
High-speed booklet folding on an automatic feeder — servo feeding, double-sheet detection and continuous delivery under load.
Watch on YouTube →04 / Review the sample
Agree the test stock, drawing, operating conditions and acceptance criteria with our team. The checks below help structure that review.
Check finished fold dimensions and print condition on the main stocks and formats in the job list.
Record setup time and sheets used for agreed changes between recurring jobs.
Confirm counting, alignment and collection against the next operation’s handling needs.
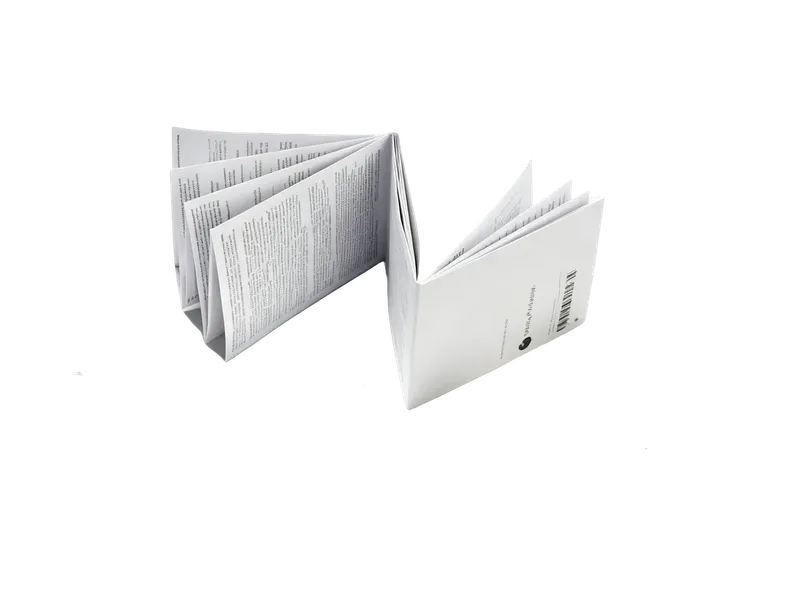
Parallel, roll and gate folds in 100–200 gsm stock, folded square enough to stack flat.
Commercial print shops alternate between brochure, catalogue and mailer formats. Fold-pattern coverage and changeover time therefore matter alongside running speed.
T490, T600 and T780 configurations cover different sheet formats. Round-pile feeding can support longer runs on compatible T600 and T780 lines. Match the plate set and feeder to the real job mix.
Parallel and cross folds for section-sewn and perfect-bound work.
Publishing signatures require stable register through parallel and cross folds so sections collate and bind cleanly.
T600 and T780 configurations address different sheet formats. A compatible round-pile feeder can reduce stops on long batches. Set the fold pattern and feeder against the actual signature stock.
An automatic paper folding machine does three things a hand-fed folder cannot: it separates one sheet at a time from a full pile, it holds that sheet in register through every fold, and it delivers a counted, squared stack at the end. Everything that decides your unit cost — how many operators you n
Solution · High-speed foldingSpeed on a folding machine is not a single number. A folder only holds its rated 180 or 210 m/min if the feeder keeps up, the rollers do not slip, and the delivery does not force a stop every few thousand sheets. High-speed folding is therefore a system question: feeder continuity, transmission type
Send the job drawing, printed stock information and production requirements. Our team can review the equipment combination and arrange the next technical discussion or sample test.
Fold-Test Sample List
Max 5 machines per fold-test request